Mild steel (MS) is the default metal of Indian fabrication. It is affordable, strong, and easy to cut, bend, and weld, which is why it shows up in everything from machine frames to gate grilles.
If you are planning a job, your real questions are probably practical: how thick can it go, how clean will the cut be, and what is it actually used for? This guide answers all three. We cover the thickness range, edge quality, and applications of mild steel laser cutting, with plain-language explanations you can use when reading a quote.
TruLight LaserTech is a fiber-laser job shop serving Delhi NCR and customers across India, so the advice here comes from the shop floor rather than a textbook.
What Is MS Laser Cutting and How Does It Work?
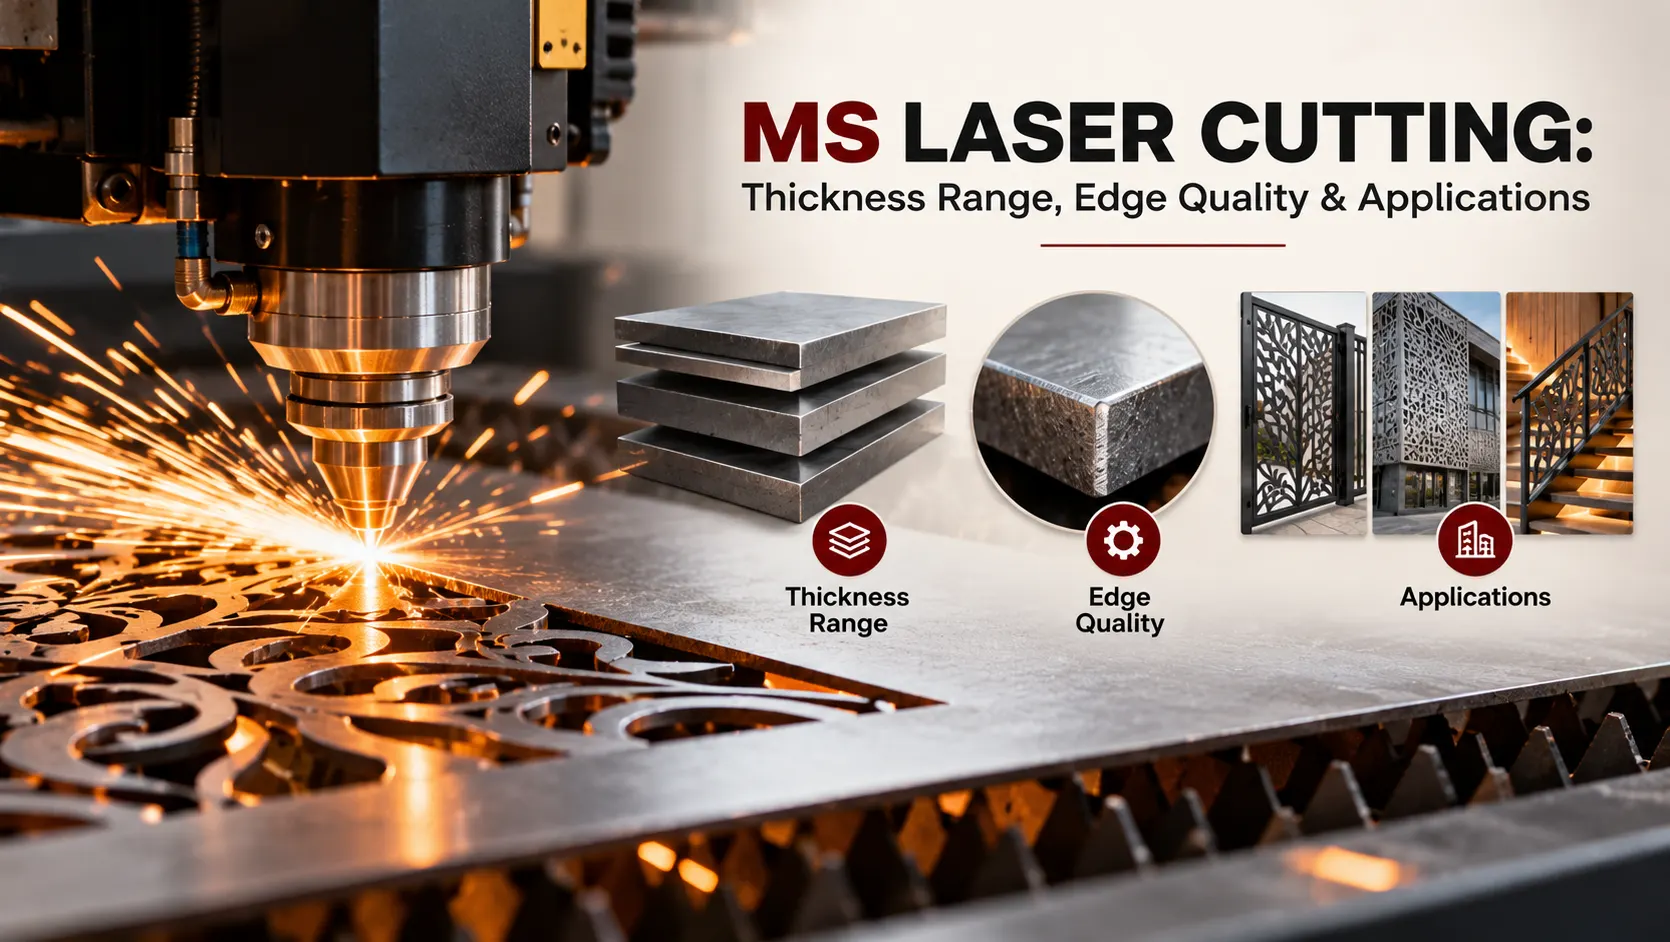
MS laser cutting is a process where a focused fiber laser beam melts a very thin line through the steel, while a jet of assist gas blows the molten metal out of the cut. The narrow strip of material the beam removes is called the kerf. Knowing this term helps later, because kerf width affects fit and finish.
Fiber lasers have largely replaced CO₂ lasers for mild steel. They cut faster on thin-to-medium gauges and cost less to run than CO₂ systems, which keeps per-part pricing competitive. Machines range from entry-level power to high-power fiber systems, and power largely determines how thick a plate can be cut cleanly.
The assist gas matters as much as the laser. Oxygen reacts with the steel and adds energy, so it cuts quickly, especially on thicker material. Nitrogen simply blows the melt away and leaves a clean, oxide-free edge.
No physical tool touches the part. That is why an intricate pattern needs no extra tooling cost to set up, unlike punching: there is no die to make, only a digital file to load. This is the core of TruLight’s CNC laser cutting service.
MS Laser Cutting Thickness Range: Sheet vs Plate
Thickness is the first thing to settle on any job, because it decides the cutting speed, the assist gas and the finish of the edge. In practice, MS is divided into sheet and plate.
MS Sheet Laser Cutting (roughly 0.5mm to 6mm)
Thin gauge is where fiber lasers are at their best. Cutting is fast, the heat-affected zone is small, and edges come off cleanest. Typical parts include electrical panels, brackets, enclosures, jali screens, and nameplates. Fine detail and small holes are realistic here.
MS Plate Cutting (roughly 6mm and up)
Thick sections call for more power and more patience. Typical jobs include base plates, flanges, gussets and structural parts, often as part of a larger sheet metal fabrication job. As thickness rises, cutting speed drops, the process usually shifts to oxygen assist, and the edge becomes coarser with more visible striations.
What Changes as Thickness Rises
Three things shift together: speed falls, the assist gas moves from nitrogen toward oxygen, and the edge finish gets heavier. There is also a practical ceiling. Most Indian fiber job shops top out around 20mm to 25mm for MS, and anything thicker usually moves to plasma or oxy-fuel cutting. At TruLight, mild steel cutting is confirmed up to 20mm.
MS Thickness Capability Table
MS Form | Thickness Band | Best Assist Gas | Typical Edge / Finish |
|---|---|---|---|
Thin sheet | 0.5-3mm | Nitrogen (or oxygen for speed) | Smooth, minimal dross, fine detail possible |
Medium sheet | 3-6mm | Nitrogen for visible parts, oxygen for general work | Clean, square edge with fine striations |
Plate | 6-12mm | Oxygen | Good edge with visible striations, oxide layer |
Heavy plate | 12-20mm+ | Oxygen | Coarser edge, oxide layer, slower cutting |
Edge Quality in MS Laser Cutting
A good laser-cut MS edge is square and shows minimal dross (re-solidified metal that clings to the bottom edge), with only fine striations (the faint vertical lines left by the cutting process). Dross and striations often come up in quotes, and knowing them helps you judge what you are being offered.
Oxygen vs Nitrogen Edges
The gas you choose is the biggest lever on edge quality, and each has an honest trade-off.
Oxygen: faster and cheaper on thick MS, but it leaves a thin oxide layer that needs cleaning before painting.
Nitrogen: gives a bright, oxide-free edge that is ready for powder coating, but the gas costs more.
Thickness | Oxygen Cut (speed / edge) | Nitrogen Cut (clean / oxide-free) | Best Use |
|---|---|---|---|
Thin sheet | Fast, slight oxide edge | Bright, oxide-free, very clean | Nitrogen for finished parts |
Medium sheet | Fast, moderate striations | Clean edge, slower and costlier | Either, depending on finish |
Thick plate | Preferred: faster, workable edge | Rarely offered; cost and gas use rise sharply with thickness | Oxygen for structural parts |
Visible / paint-ready parts | Needs edge cleaning first | Ready for powder coat | Nitrogen |
What Ruins Edge Quality
Even a good machine can produce a poor edge. The usual culprits are dirty or rusty stock, incorrect focus, a worn nozzle, or cutting speed set too high. A reliable shop controls all four.
Tolerance and Squareness
Typical fiber laser tolerance is near ±0.1mm on sheet. It is a little looser on thick plate, where the cut face is less perfectly square. For an objective benchmark, thermal-cut edges are graded under ISO 9013, so you can specify the edge grade you need instead of relying on a vague “good finish”.
Is MS the Same as Carbon Steel? Material and Grades
People searching for carbon steel laser cutting often wonder whether it is a different job from MS. It is not. Mild steel is low-carbon steel, which makes it a sub-type of carbon steel. To put it plainly: all mild steel is carbon steel, but not all carbon steel is mild. “Mild” means low carbon, roughly under 0.25 percent.
If you searched for carbon steel laser cutting, the same fiber-laser process applies.
In India, the common structural grade is IS 2062 (E250), while ASTM A36 often appears on export work. Carbon content matters because higher-carbon steels can harden at the cut edge and behave differently when bent or machined afterwards.
Property | Mild Steel (low carbon) | Higher-Carbon Steel |
|---|---|---|
Carbon content | Roughly under 0.25% | Higher |
Edge behaviour | Cuts cleanly, easy to bend and weld | Edge may harden, affecting later bending or machining |
Typical use | General fabrication, structures | Springs, tools, wear parts |
For deeper grade questions, see the FAQs below.
MS Laser Cutting Designs and DXF Files
Design quality drives part quality. A clean vector file lets the laser follow exact paths, which is what makes cuts accurate and repeatable.
Most job shops accept DXF and DWG as standard, with PDF useful as a reference. Popular MS design categories in India include jali and grille patterns, gates, railings, nameplates, signage and brackets.
Two practical design rules help parts cut cleanly:
- Keep the smallest feature roughly equal to the material thickness. A 6mm plate should not carry 2mm holes.
- Avoid over-fine detail on thick plate, and use small bridge tabs so delicate inner pieces hold together.
No DXF? TruLight offers in-house 3D modelling and design support, so you are not stuck without a file.
Applications of MS Laser Cutting
The same process serves very different industries.
- Automotive and auto-components: brackets, chassis parts and enclosures cut in volume with repeatable accuracy.
- Construction and infrastructure: base plates, cladding panels, structural gussets and handrails.
- Decorative and architectural: jali screens, gates, signage and furniture frames.
- Industrial and electrical: control panels, cabinets, machine parts and mounting plates.
A Delhi NCR job shop typically serves OEMs, contractors and signage firms, each with different priorities: volume and consistency for OEMs, structural strength for contractors, and visual finish for signage.
This variety comes back to the two pillars covered earlier. Thickness flexibility lets one process handle a 1mm panel and a 20mm base plate, and edge quality decides whether a part is ready to paint or needs more work.
Choosing an MS Laser Cutting Service in India
Before sending a job, check the basics: laser power, bed size, maximum thickness, tolerance and turnaround. Turn the technical points above into buyer questions. Can they hold my tolerance? Can they cut my thickness? Will they dispatch on time?
Also look at value-adds that save you a second vendor, such as CNC bending, powder coating and design support.
TruLight LaserTech cuts mild steel up to 20mm on fiber lasers and offers in-house CNC bending and powder coating. Most jobs are dispatched within 24 hours, from Delhi NCR to customers Pan-India.
Conclusion
MS laser cutting spans everything from thin sheet to roughly 20mm plate, with clean edges near ±0.1mm, serving automotive, construction, decorative, and industrial work. The right cut comes from matching thickness, assist gas, and tolerance to the job, and a good job shop will sort that out for you.
Ready to start? Send a DXF or drawing to TruLight and get a quote. Explore our MS Laser Cutting and Sheet Metal Fabrication pages for more information.
Frequently Asked Questions
How thick can a laser cut mild steel?
Modern high-power fiber lasers handle MS up to roughly 20-25mm. Thicker material usually shifts to plasma or oxy-fuel cutting.
How much does MS laser cutting cost per sq ft in India?
It varies by thickness and quantity. Ask for a drawing-based quote rather than relying on a flat rate.
Is mild steel the same as carbon steel?
Mild steel is carbon steel, specifically the low-carbon kind with under about 0.25 percent carbon.
Fiber or CO₂ laser for mild steel, which is better?
Fiber wins on thin-to-medium MS for speed and running cost. CO₂ is now largely superseded for most MS work.
Oxygen or nitrogen assist gas for MS?
Oxygen for speed on thick plate. Nitrogen for a clean, paint-ready, oxide-free edge.
What tolerance can MS laser cutting hold?
Typically around ±0.1mm on sheet, and a little looser on thick plate.
Does laser-cut mild steel need deburring?
Usually minimal. Nitrogen edges are near ready to use, while oxygen edges may need light cleaning before paint.